Short Answer
Refinery turnaround scaffold planning starts with a detailed scope walk and billable-hour analysis, continues through material takeoffs including toeboard counts, moves into crew sizing and erection sequences, and closes with pre-use inspection tagging and teardown. A one percent schedule slip on erection or inspection can cost a day or more of the shutdown window.
Refinery turnarounds are precision events: a shutdown window of 10 to 30 days, multiple contractors in confined spaces, and no schedule slippage allowed. Scaffold planning is the critical path that everything else hangs on. Get the scope, the material counts, and the crew sequence right the first time, and the turnaround keeps its pace. Guess, and a single erection delay can cascade into lost days and six-figure costs.
How to Conduct a Scope Walk for a Refinery Turnaround
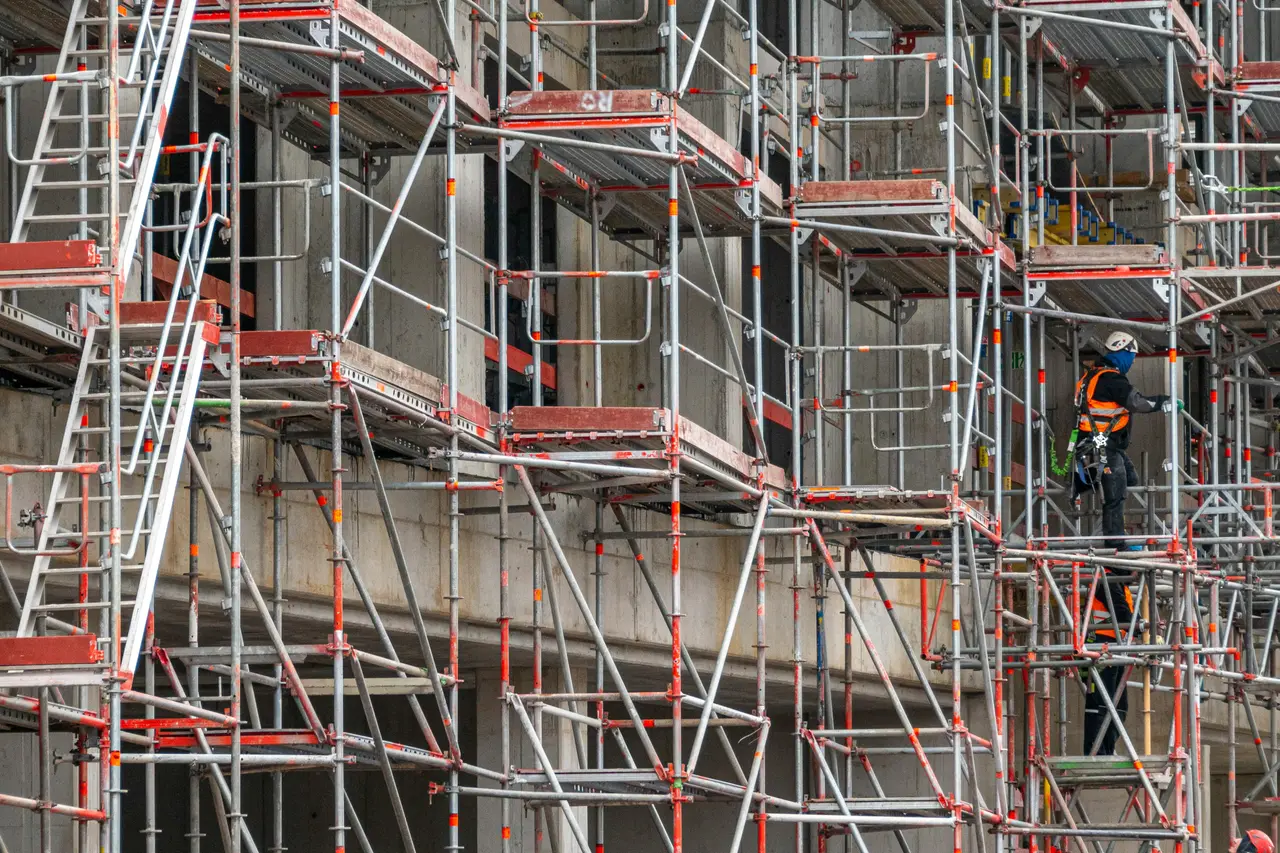
The scope walk is not a construction meeting. It is a legal and technical fact-finding mission. Bring the plant HSE director, your lead erector or competent person, the turnaround manager, and a crane or equipment coordinator (if heavy rigging is involved). Walk every platform, every vertical rise, every access stairway, and every work zone.
Mark the erection sequence on a floor plan as you go: which zones get built first, which depend on others being up, and where the critical-path items are. Identify every tie point for lanyard and load rigging (required under 1926.451 for competent-person authority and employee protection). Mark every walkway that will be blocked by scaffold or material. Photograph every zone with a date stamp and crew names. That record becomes your baseline if a later change request or delay dispute arises.
At the same time, count the toeboard zones. Under 29 CFR 1926.451(h)(2)(ii), a toeboard is required along the edge of platforms more than 10 feet above lower levels. Count the linear feet of edge that needs a toeboard, note whether the plant has a material-stacking limit above the toeboard (some refinery specs require paneling to the guardrail), and confirm which toeboard attachment method the plant’s scaffold spec allows. The choice between tie wire, wood blocking, and a bracket system directly affects your erection pace.
Material Takeoff: The Numbers That Drive the Schedule
Once the scope walk is complete, the material takeoff is a column-by-column inventory of every component needed. For a tube-and-clamp or ring-lock scaffold, this is standard: how many tubes of each length, how many couplers, how many base plates, how many guardrail components. But toeboards are often miscounted or forgotten entirely, which then hits the schedule during erection.
Toeboard Takeoff Formula
Count the linear feet of platform edge requiring a toeboard. Divide by the span of your toeboard boards (typically 8 to 10 feet). That is your board count. Then, count the attachment points (standard is every 4 feet, per 1926.451(h)(4) fastening requirements). Multiply by three: one for the original installation, one for breakdowns or damage on site, and one for spare capacity in the high-traffic zones.
For a 4,000 linear-foot project:
- Linear feet needing a toeboard: 4,000
- Board span (8 feet): 500 boards
- Spare factor (30 percent): 150 boards
- Total: 650 boards
If you are using 2x4 lumber, source graded lumber (scaffold grade) and confirm it meets the plant’s inspection standard. If you are using a bracket system like Diamond Deck, confirm the board pockets fit your lumber or metal toeboard size, and order enough brackets for the linear feet plus 25 percent spare.
Erection Material Schedule
Factor the toeboard materials into the critical-path timeline. Fastening method changes the per-board time: #9 tie wire and wood blocking (the traditional method) takes longer per board than a bracket system with set screws, though the exact minutes depend on your crew and site conditions. Use the labor and material cost calculator to model your crew size, board count, and toeboard method against your specific scaffold system and see the schedule impact for your project.
Crew Sizing and Erection Sequence
A crew of two erectors can build 200 to 400 linear feet of platform per day on frame or tube-and-clamp systems, depending on platform height, complexity, and toeboard fastening method. Ring-lock and Cuplock systems run slightly faster because the couplers lock without hand tightening.
Divide the total linear footage by the crew’s daily rate. Add 20 percent for weather, material delays, and learning curve on the specific scaffold system the plant uses. Then, add time for competent-person inspection. At most refineries, the competent person must tag every completed section before the next crew shift uses it. A competent person inspecting and tagging completed scaffold can cover 300 to 500 linear feet per day. If the plant requires daily tagging, that is a second bottleneck: erection and inspection cannot fully overlap.
For a 4,000 linear-foot project:
- Erection at 300 linear feet per day: 13 days
- Inspection tagging at 400 linear feet per day: 10 days
- Total with 20% buffer: 14 to 16 days
Toeboard fastening method affects daily erection pace: wire-and-blocking adds more time per 100 linear feet than a bracket system with set screws. Run your own board count and crew pace through the labor and material cost calculator to see the schedule impact on your erection window.
Inspection, Tagging, and Load Verification
Before any employee works on the scaffold, the competent person must inspect the entire assembly. Inspection covers base plates, tube alignment, coupler tightness, guardrail height and gaps, toeboard height and fastening per 1926.451(h)(4), and any diagonal bracing or tie points required by the system manufacturer or the design engineer.
Each completed section receives a tag with the competent person’s initials, the inspection date, and the next re-inspection date (usually 7 days for ongoing use). Photographs of each tagged section protect both the contractor and the plant in case of a later inspection challenge.
If the plant also requires load-verification of the platform (test load before work begins), add another shift or more. Load testing typically uses steel plates, sandbags, or water weights staged on the platform until it reaches the design load (usually 1.5 to 2 times the intended working load). The competent person monitors for deflection, movement, or noise, then signs off. This step is rare on routine turnarounds but common on new scaffold designs or modifications.
Teardown and Demobilization
Once the turnaround work is complete, the scaffold comes down. Demob runs 50 to 70 percent the erection pace because the crew can work without the precision constraints of new work. Material is removed, not installed, so speed increases.
Sequence the teardown to avoid trapping material or creating hazards. Remove toeboards first, working section by section so workers are never blocked. Then remove the guardrail, then the platform frames or ring-lock ledgers. Finally, remove the uprights and base plates. All hardware is inspected for damage or wear and loaded for transport or storage.
For that same 4,000 linear-foot project: if erection took 14 days, demob typically takes 8 to 10 days. Material is trucked out as it comes off, so rental equipment can be returned on schedule.
Where Toeboard Method Affects the Critical Path
The toeboard fastening method is often the hidden variable in scaffold schedules. Traditional wire-and-blocking is labor-intensive but familiar to most crews. A bracket system cuts the labor and schedule, but requires the system to be designed and the brackets to be on site and compatible with the scaffold tubes and boards in use.
For a refinery turnaround, where a one-day erection slip cascades into lost shutdown hours, the toeboard choice can accelerate or delay the entire schedule. If you are planning a turnaround and toeboard fastening is not yet specified, ask the plant’s HSE and scaffold specs team: “Is a bracket system an option?” The answer drives crew size, material cost, and the erection timeline.
Diamond Deck is a steel toeboard bracket that clamps to the vertical tube and holds two toeboards in adjustable pockets with set screws, no tie wire or wood blocking. Designed to the toeboard requirements of 29 CFR 1926.451(h)(4), with load testing and Professional Engineer review in progress, it can cut toeboard installation time on projects where the plant allows bracket systems in place of traditional fastening. Fit testing with major scaffold systems is in progress.
The upfront planning and material discipline turn a refinery turnaround scaffold project from a crisis into a sequence. Get the scope walk right, count the toeboards accurately, size your crew for the toeboard method, and build in competent-person inspection time. A 10,000 linear-foot turnaround with precision planning comes together on schedule. Without it, you are firefighting.
Ready to plan your refinery turnaround scaffold? Start with an accurate scope walk and a material takeoff. For the toeboard-specific counting method, see estimating scaffold accessories for a job. Request a quote for toeboard hardware, consultation on crew sizing, or submittal documentation for your project specifications. Get a quote today.
Frequently Asked Questions
How Do You Plan a Refinery Turnaround Scope?
The scope walk is led by the plant HSE director and includes the scaffold contractor, the competent person, the turnaround manager, and a crane or equipment coordinator. Walk every platform, every access point, every work zone, and mark every lifting tie point, every blocked walkway, and every zone where materials will land. Mark the toeboard zones at the same time. A photo record with a date and crew names anchors the scope.
How Many Toeboards Do I Need for a Refinery Turnaround?
Count the linear feet of platform edge above 10 feet, per 29 CFR 1926.451(h)(2)(ii). Divide by the toeboard span (usually 8 to 10 feet). Then add 50 percent for corners, offsets, and breakdowns on site. Toeboards must be securely fastened per 1926.451(h)(4) and fit the system scaffold and board standard in use.
What Crew Size Is Typical for Scaffold Erection?
A crew of two erectors per 200 to 400 linear feet per day is typical for frame or tube-and-clamp systems. Ring-lock and Cuplock systems run slightly faster. The pace depends on platform height, access, soil conditions (for base plates), tie rigging, toeboard fastening method, and crew experience with the specific system. Add time if the competent person requires daily inspection tagging before the next shift.
How Long Does It Take to Inspect and Tag Refinery Scaffold?
A competent person inspecting and tagging a completed scaffold at a refinery can cover 300 to 500 linear feet per day, depending on system complexity, toeboard fastening scrutiny, and the plant's photo and tag format. Add time if toeboards are tied with #9 wire (labor-intensive) vs. a bracket system. Turnaround schedules often build in a full shift or more for inspection and re-touch before the first work day.
What Does the Teardown and Demobilization Timeline Look Like?
Demob typically runs one half to two-thirds the erection pace, because the crew can work without the precision or rigging constraints of new work. A 4,000 linear-foot project with a 10-day erection schedule usually comes down in 5 to 7 days, including toeboard removal, hardware inspection, load verification, and truck-out. Sequence the toeboard removal to avoid trapping material on the platform.